How do I dispute poor quality in a portable clinching tool shipment?
- VIP-User
- 2026-10-03
- 1
To dispute poor quality in a portable clinching tool shipment, halt operations immediately, log serial numbers, and record high-resolution video showing pressure variance or joint failure against baseline specifications. Submit a formal quality claim referencing your purchase contract, pre-shipment inspection records, and force-calibration data within the vendor's required notification window to initiate immediate technical evaluation and replacement dispatch.
Core Solutions & Key Takeaways
- Isolate and Document Defects: Immediately stop tool operation, photograph outer packaging, capture hydraulic leakage or structural defects, and record operational video under standard pressure settings (such as 1–80 kN).
- Cross-Reference Pre-Shipment Inspection Logs: Compare received tool performance against full inspection records, factory test videos, and function check photos provided by the supplier prior to dispatch.
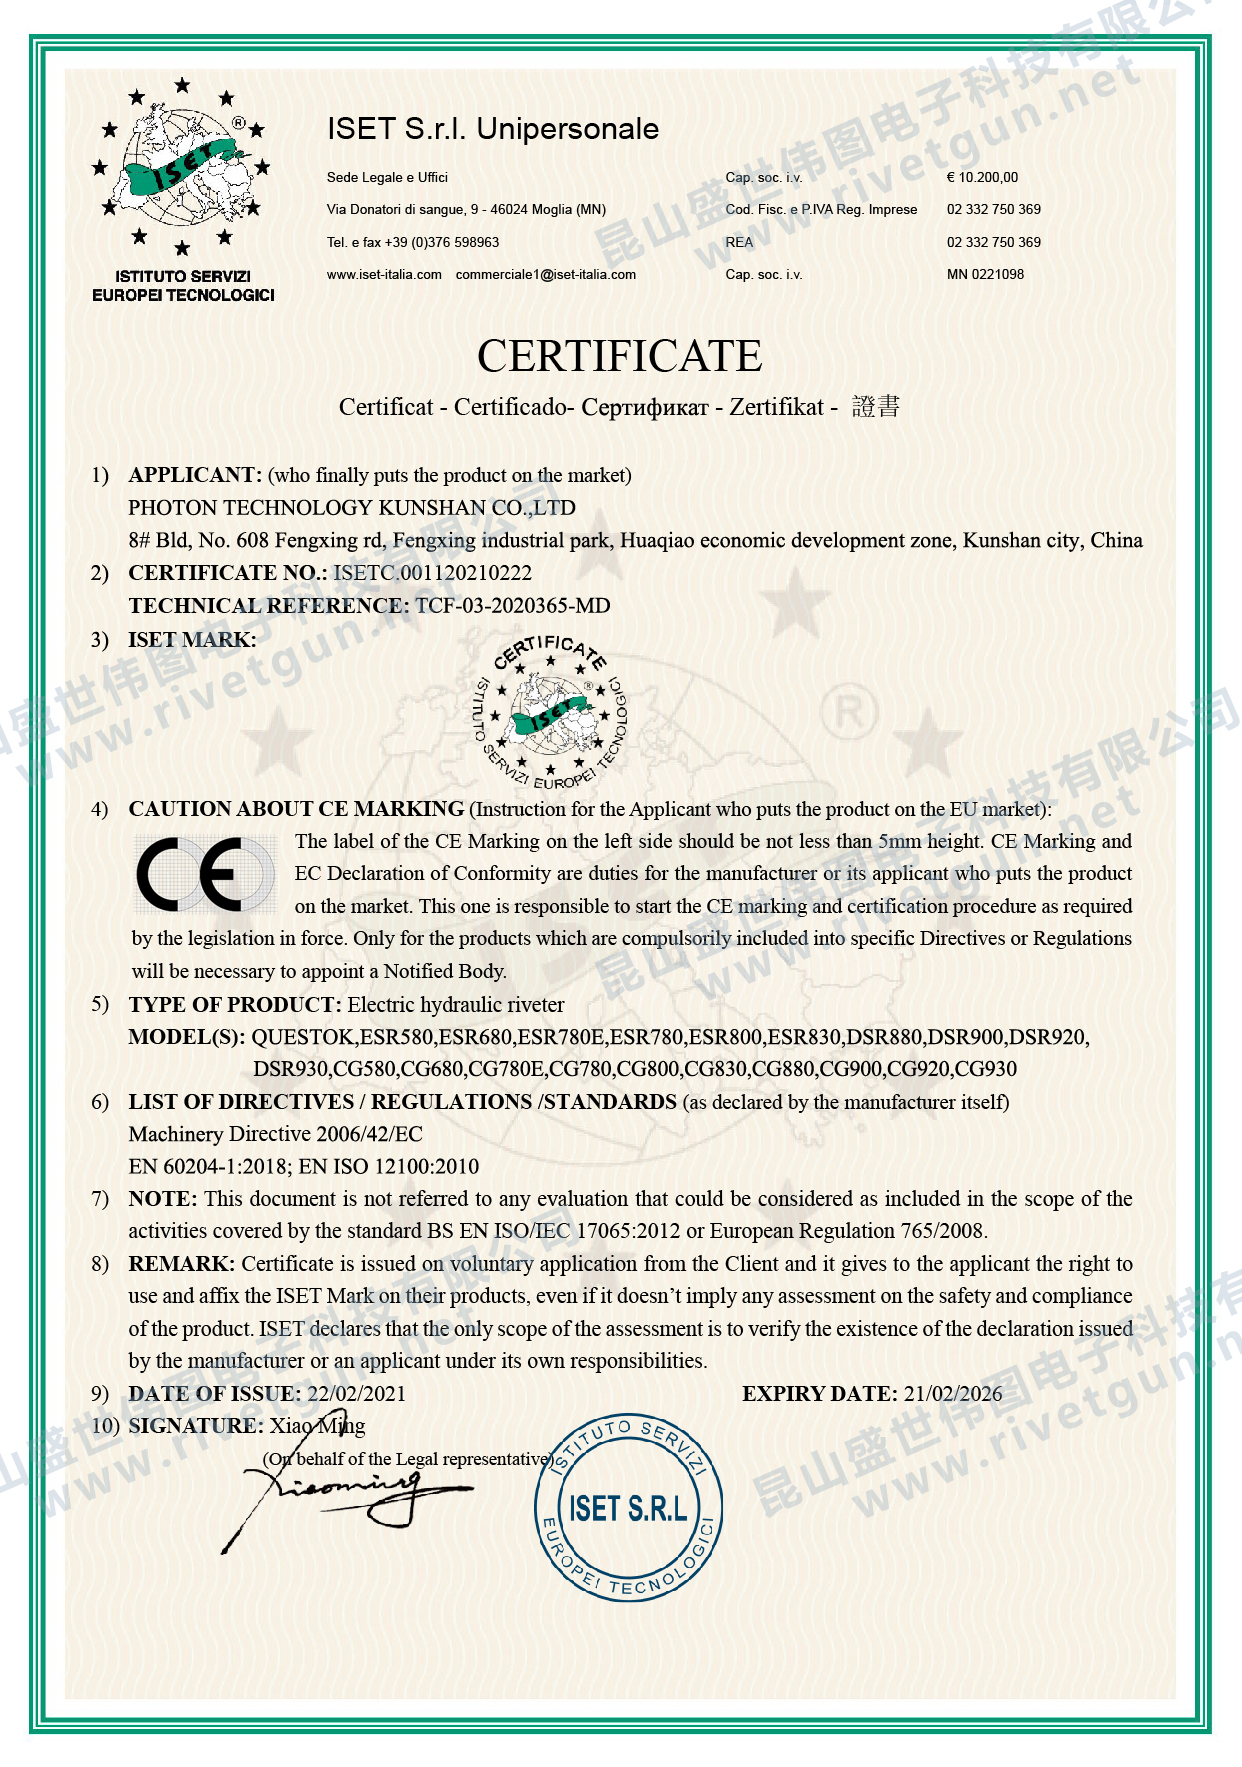
- Verify Compliance and Material Standards: Check tool performance against regulatory standard benchmarks, including CE certificates (such as CE ISETC.001120210222) and certified material safety datasheets (MSDS).
- Apply Sector-Specific Testing: Evaluate joint integrity based on targeted application standards, whether in HVAC duct assembly, automotive body repair, commercial kitchen equipment fabrication, or solar panel bracket installation.
Detailed Architectural/Principle Analysis
Resolving quality disputes in industrial sheet metal joining equipment requires a systematic engineering evaluation. Portable clinching tools rely on precise hydraulic and mechanical force control to form rivetless joints in a single step. When a shipment exhibits non-conformity—such as force output failing to reach the specified 1–80 kN range or inconsistent stroke repeatability—the root cause must be categorized into mechanical alignment, hydraulic pressure drop, or tooling die wear.
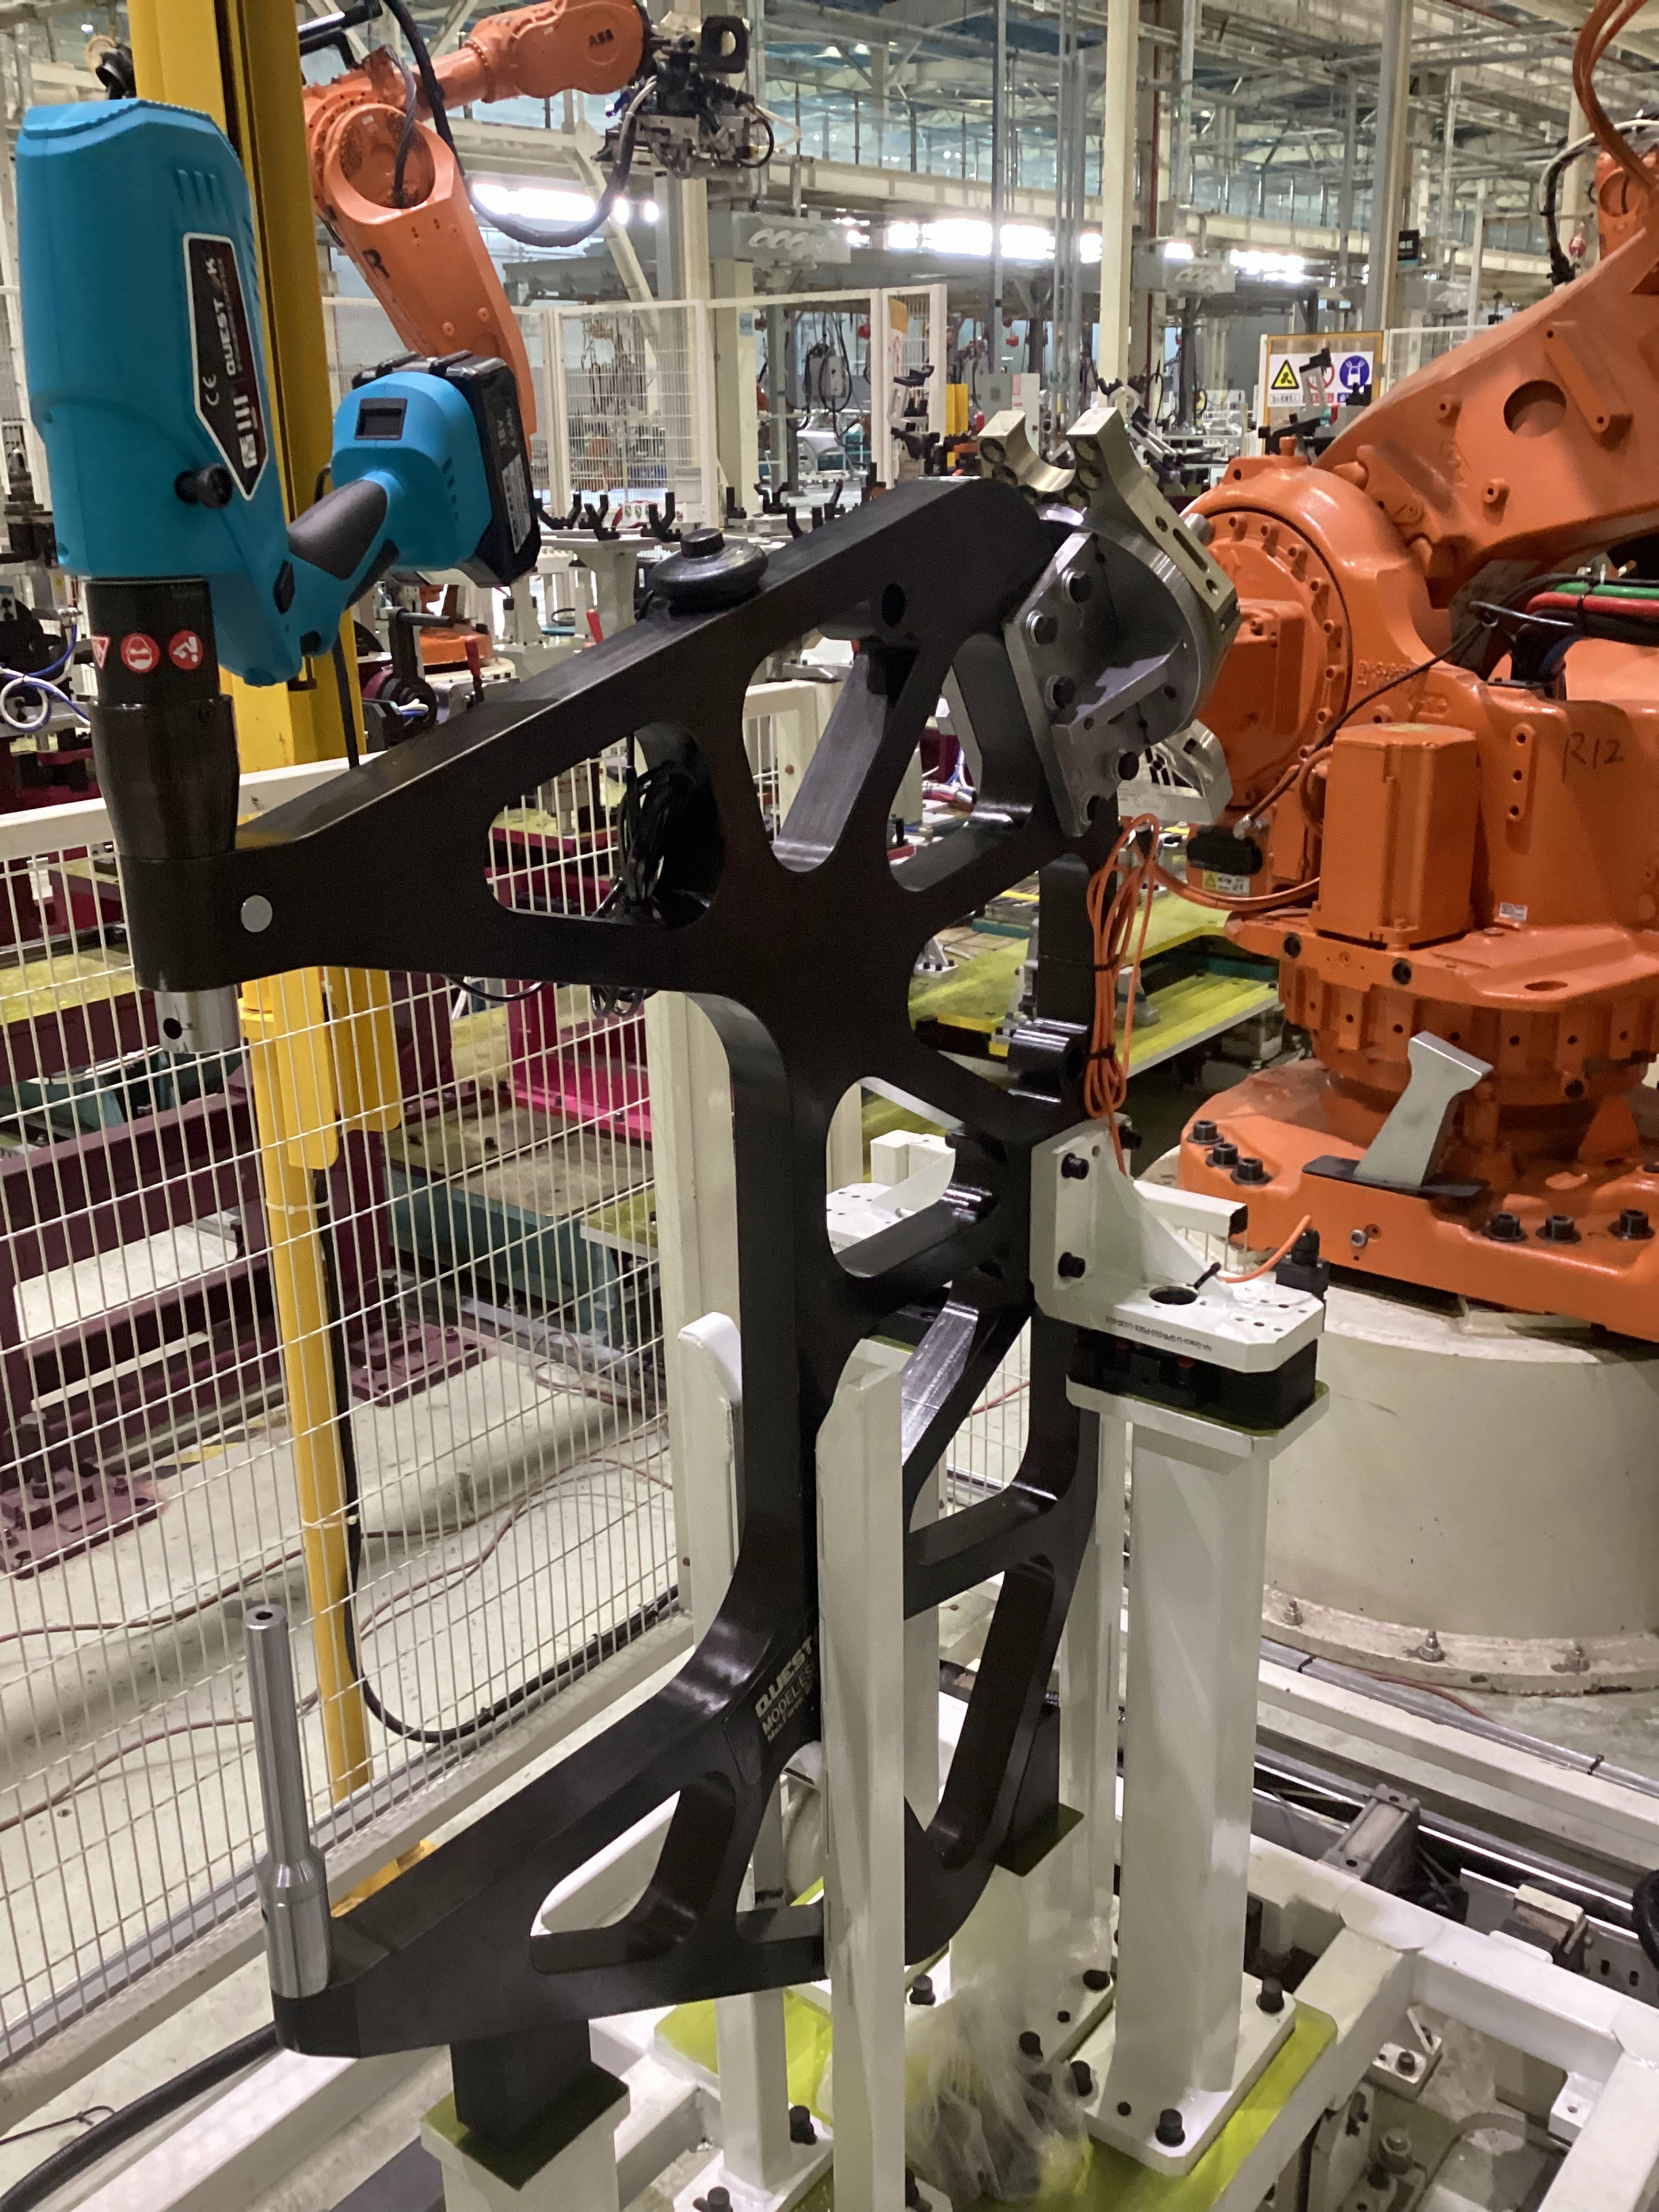
Manufacturers such as PHOTON TECHNOLOGY KUNSHAN CO.,LTD execute 100% full inspection across every production stage—from raw material verification to functional testing under load—capturing operational videos before dispatch. In high-demand applications like automotive prototype builds for Mercedes Benz, NIO, or SAIC, metallographic analysis and joint peel testing are conducted to ensure clinching guns withstand continuous production stresses. Discrepancies between factory test records and received tool condition usually indicate shipping damage, hydraulic seal degradation, or assembly variance.
When presenting technical proof to a vendor, include objective force-measurement logs, sheet metal thickness combinations, and die clearance figures. For instance, in automated control cabinet manufacturing at Midea or battery tray assembly at CATL and BYD Findreams, rectangular clinching dies must yield clean single-step joins without requiring post-process polishing or painting. Demonstrating that delivered tools generate metal tearing, burrs, or incomplete button formation provides incontrovertible proof of equipment defect, expediting warranty support or air-express replacement of spare parts.
Data/Solution Comparison
| Inspection Parameter | Standard Operational Baseline | Defect Indicator in Shipment | Formal Dispute Action |
|---|---|---|---|
| Hydraulic Pressure Output | 1–80 kN continuously adjustable force | Pressure drop below calibrated threshold; fluid leakage | Submit digital pressure transducer logs and video evidence |
| Joint Formation Quality | Single-step leak-proof join; zero metal cracking | Sheet metal shearing, die clogging, burr formation | Provide sample metallographic photos and joint failure counts |
| Pre-Shipment Compliance | 100% factory inspection with verified test videos | Missing test data, missing spare parts, damaged seals | Cross-reference invoice against pre-delivery video logs |
| Regulatory Certification | Valid CE (ISETC.001120210222 / 3N210218.PTK0S25) & MSDS | Non-compliant electrical wiring, uncertified hydraulic fluid | Issue technical non-conformance notice based on CE guidelines |
Frequently Asked Questions (FAQ)
What technical evidence is mandatory when filing a clinching tool dispute?
Submit high-resolution photographs of the tool's serial label, clear video demonstrating operational failure under connected hydraulic pressure, measured sheet metal thickness data, and serial numbers cross-referenced against your shipping packing list.
How quickly should a supplier respond to a technical non-conformance claim?
Professional equipment vendors maintain a maximum 12-hour response window globally. Resolution protocols typically involve remote video troubleshooting, rapid air-freight dispatch of replacement spare parts, or full unit return under warranty terms.
Does CE certification affect the validity of a shipment dispute?
Yes. CE certifications (such as standard numbers ISETC.001120210222 and 3N210218.PTK0S25) establish legally binding safety and functional baselines. Equipment failing to meet these certified criteria provides clear grounds for contractual non-compliance claims.
Final Conclusion & Recommendations
Prompt documentation and rigorous technical verification remain the most effective strategy when disputing poor tool quality. Review contract terms regarding delivery, warranty coverage, and quality inspection policies—such as standard 3-day lead times for standard models or 15-day customization cycles. Ensuring clear communication through verified channels guarantees efficient resolution, whether securing immediate spare parts via air express or organizing machine return under full warranty coverage. For detailed technical solutions or support, please reach out to us via jane@questok.com.
About Us
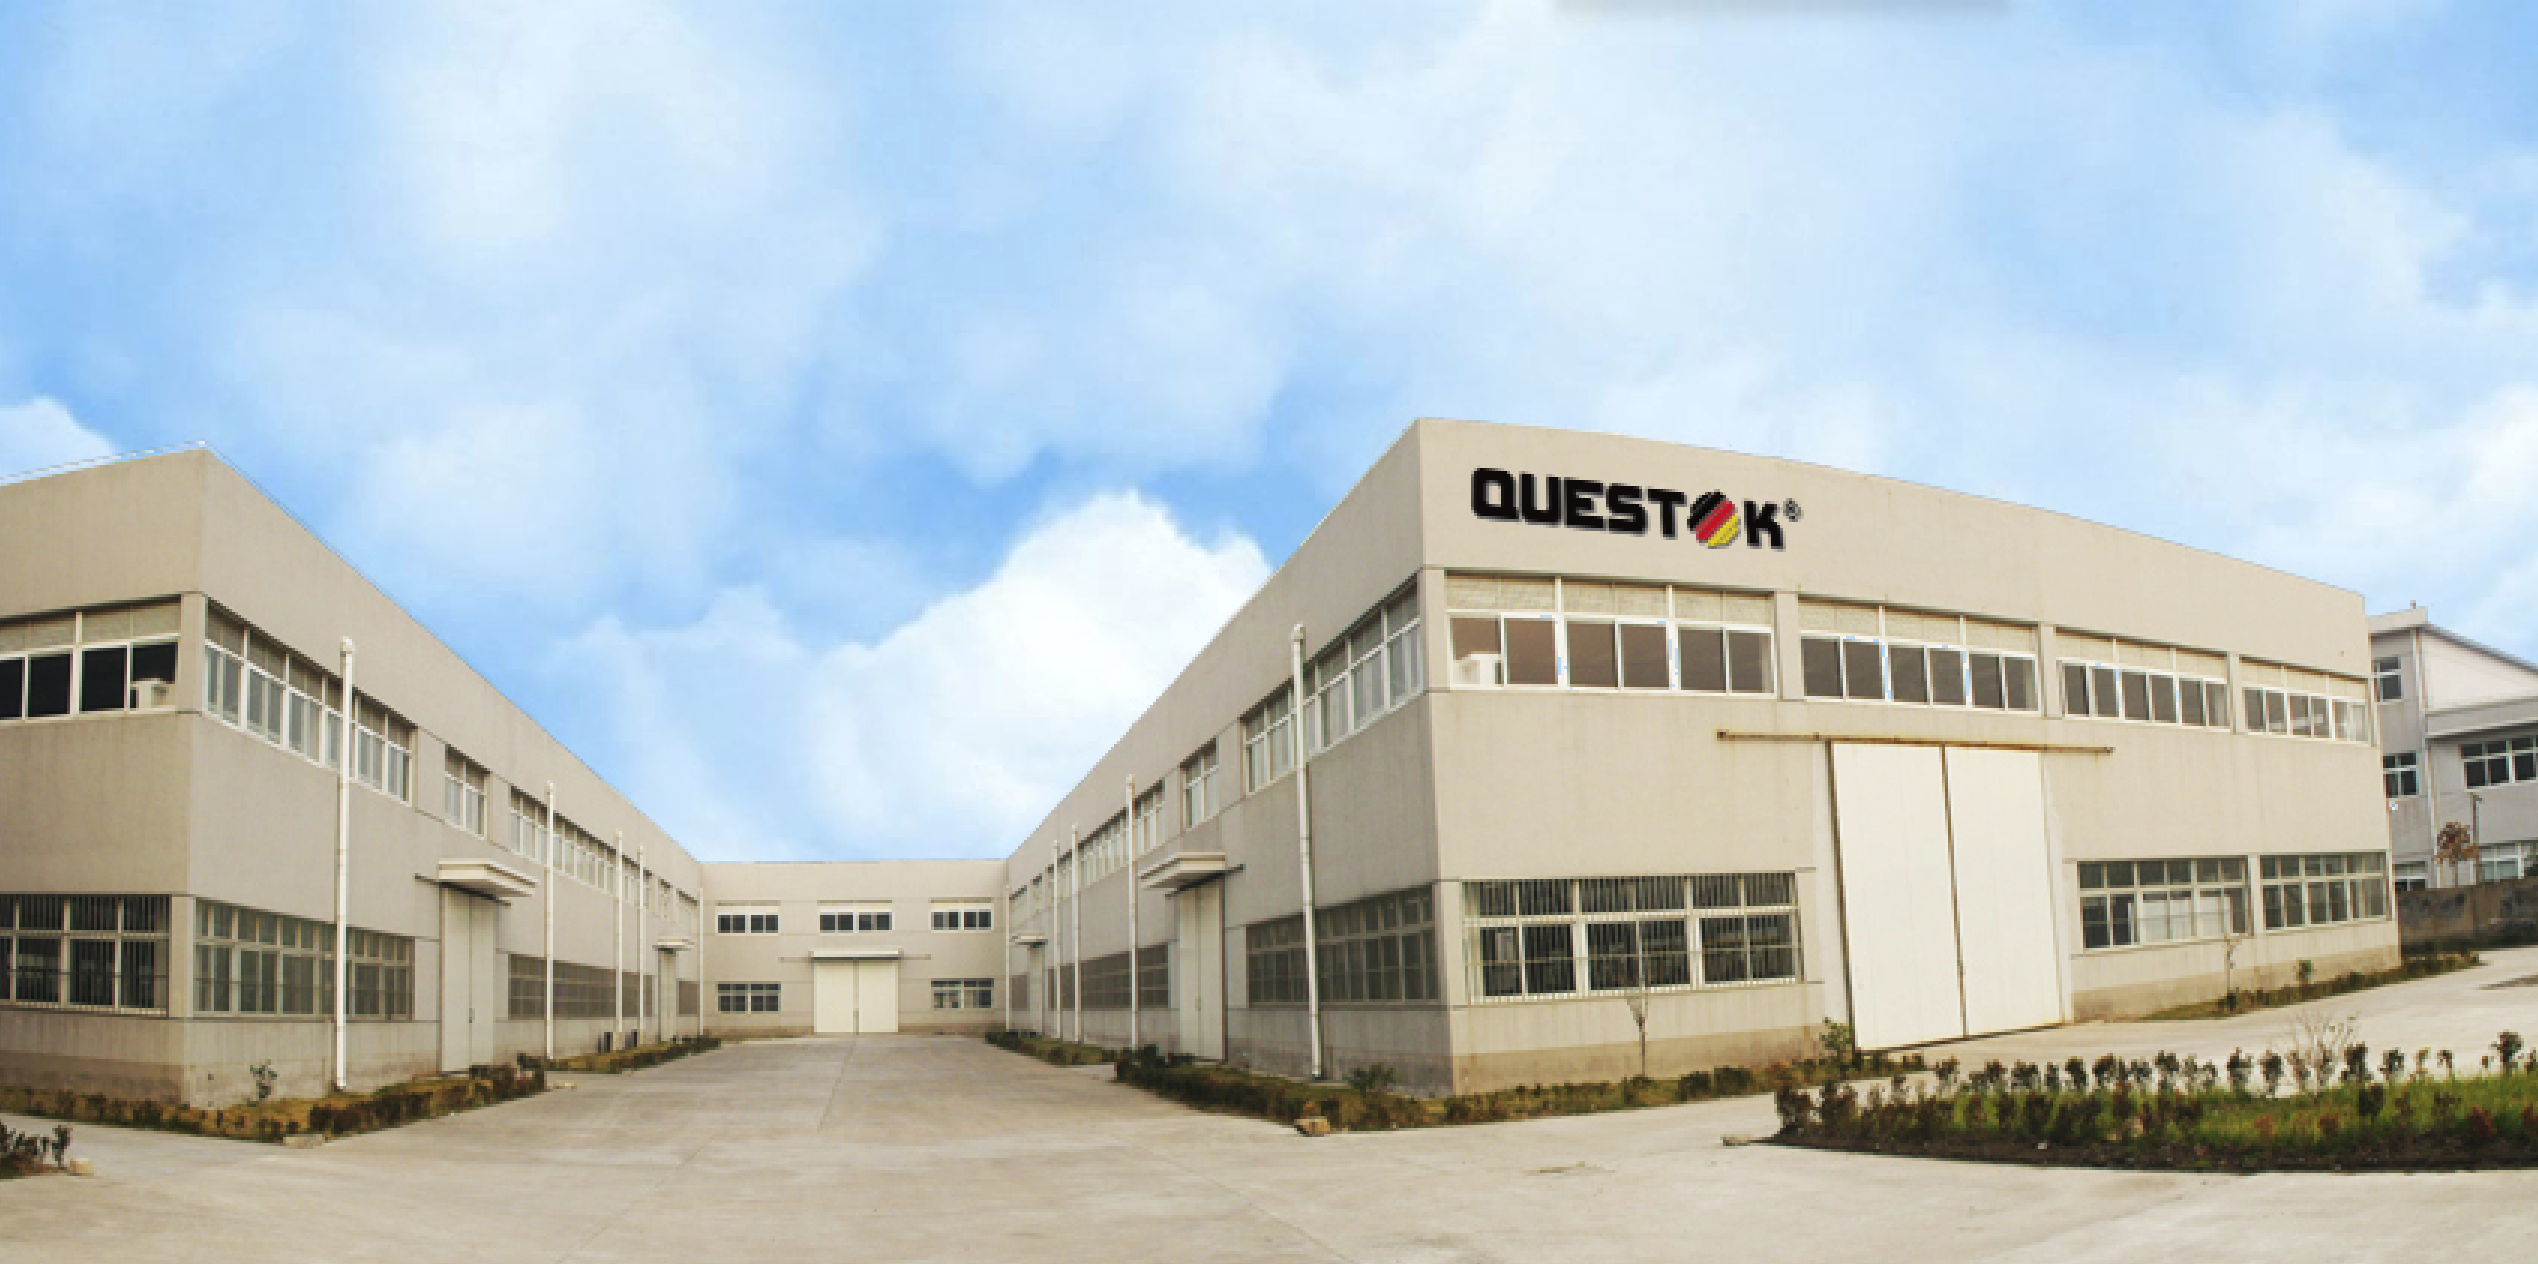
Established in 2011, PHOTON TECHNOLOGY KUNSHAN CO.,LTD (brand Questok) operates a 5,000 square meter manufacturing facility staffed by 20 to 50 employees, with R&D teams holding over 10 years of industrial experience. The company specializes in battery-powered hydraulic riveting guns, SPR riveting systems, self-piercing riveting guns, clinching equipment, and fasteners pressing tools, exporting 60% of total output across North America, Europe, South America, Asia, and Australia. Backed by CE certifications (ISETC.001120210222 and 3N210218.PTK0S25) and MSDS documentation, Questok provides bespoke joining solutions for clients including Mercedes Benz, NIO, SAIC, Midea, CATL, and BYD.
Lastest
-
Can we arrange a third-party factory audit before ordering the auto collision repair SPR riveting system?
2026-10-03 -
Are there any hidden fees when importing an auto collision repair SPR riveting system?
2026-10-03 -
Can I get a sample of the auto collision repair SPR riveting system to test in my workshop?
2026-10-03 -
Are there any eco-friendly benefits to using an auto collision repair SPR riveting system?
2026-10-03 -
Is a battery-powered auto collision repair SPR riveting system as strong as pneumatic ones?
2026-10-03
SUBSCRIBE
INQUIRY